Capabilities
Built for manufacturers. Ready for your product.
Conveyors, cranes, gearboxes, process plant, tooling and steel doors first. One platform and one method for every product: your rules are added once, then every order is designed, drawn, listed and priced the same way.
The periodic table of configurable products
240 product families. One way of working.
20 manufacturing sectors, twelve families each. Search it, filter it, or bring something that is not here yet. The 31 blue tiles open as live 3D in the platform on our home page.
Not on the list? Tell us what you build. If it follows rules, we can automate it.

Conveyors and material handling.
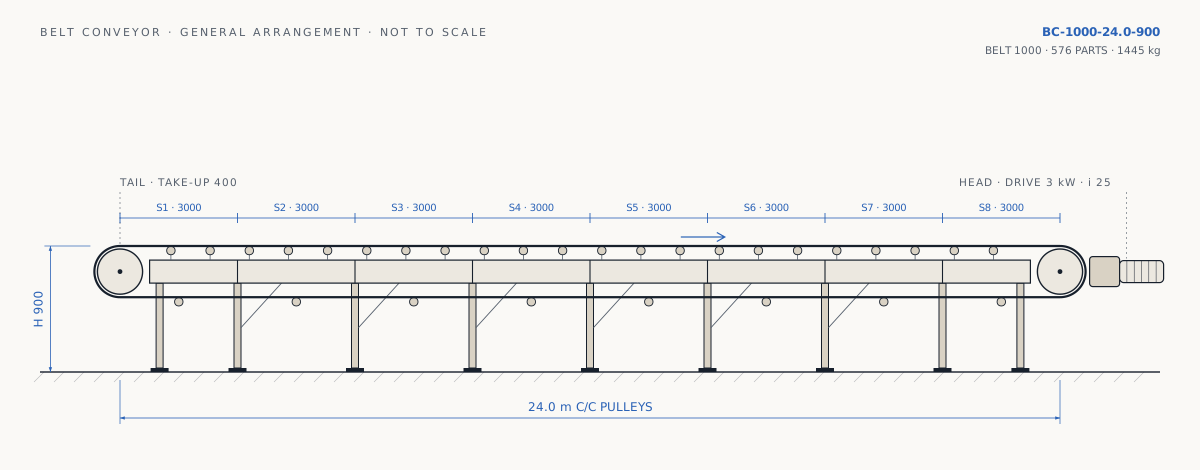
Every belt, roller and chain conveyor is a chain of decisions. One length change ripples through sections, legs, idlers, belt, drive and guards. Your designers redo that chain by hand on every order. The platform does it in milliseconds and draws the general arrangement.
Length 12 → 24 m: frame sections 4 → 8, support legs 10 → 18, carry idlers 10 → 20, belt 25.6 → 49.6 m, drive motor 1.5 → 3 kW, and the parts list grows from 286 to 556.
What we automate
| Output | For |
|---|---|
| General arrangement | Customer approval |
| Frame and leg drawings | Fabrication |
| BOM and cut lists | Purchasing |

Cranes and lifting equipment.
Double-girder and single-girder overhead cranes, gantries and jib cranes are different structures, each sized by span, lift and load. One number moves girder depth, wheelbase, wheels, motors, rope and the runway. Goods and passenger lifts follow the same method: load sets the car, the car sets the shaft, travel sets the speed.
Span 16 → 30 m and 10 → 50 t: girder depth 900 → 2400 mm, gauge 1.6 → 2.7 m, wheelbase 2.6 → 4.6 m, wheels Ø400 → Ø710, hoist 11 → 55 kW, rope Ø11 → Ø25, wheel load 82 → 350 kN, runway HEA 300 → HEB 600.
What we automate
| Output | For |
|---|---|
| General arrangement drawing | Customer and civil |
| Girder and end-carriage fabrication | Workshop |
| Wheel-load and calculation sheet | Approval |

Gearboxes and power transmission.
Helical reducers, two-stage gearboxes and worm gear units are a ratio, a torque and a service factor. They set the centre distances, the gear stages, the shafts and bearings, the housing, the oil and the thermal check, and the drive package around them: motor, coupling, guard and baseplate.
Helical reducer, 7.5 kW at ratio 4, service factor 1.0 → 1.5: design torque 192 → 287 N·m, centre distance 80 → 100 mm, gears 21:84 → 26:104, output shaft Ø32 → Ø38, bearing 6208 → 6209, oil 1.0 → 1.6 L, mass 20 → 35 kg.
What we automate
| Output | For |
|---|---|
| Gearbox arrangement and data sheet | Customer |
| Housing, shaft and gear drawings | Machining |
| Gear and bearing calculation sheet | Engineering approval |

Process plant, valves and piping.
Vessels, pumps, valves and the piping between them are one system. Vessel and line size decide the nozzles, the pump power, the pipe route, every elbow, flange and bolt, the valves on each line and the supports under them.
Pump skid, Ø1.6 × 3 m vessel on DN 80, one pump → two (duty and standby): pipe routed 12.3 → 17.1 m, valves 8 → 11, flanged joints 18 → 26, bolts 144 → 208, welds 38 → 54, mass 3.1 → 4.0 t.
What we automate
| Output | For |
|---|---|
| Line list and pipe isometrics | Piping and fabrication |
| Valve, flange and bolt schedule | Purchasing |
| Skid arrangement and BOM | Fabrication and site |

Moulds, dies and fixtures.
Injection moulds, progressive dies, roll-forming tooling, jigs and fixtures are standard parts arranged by rules. Cavities set the mould base, strip width and stations set the die set, bends and thickness set the forming stands, and the part sets the locators, clamps and bushes of its fixture. The toolroom quotes and draws them in hours, not weeks.
Progressive die, 50 → 180 mm strip and 4 → 9 stations: die set 320 × 230 → 1246 × 378 mm, punches 6 → 11, guide pillars Ø25 → Ø40, springs 12 → 22, cutting force 185 → 1497 kN, press 25 → 200 t.
What we automate
| Output | For |
|---|---|
| Mould and die assembly | Toolroom |
| Plate and insert drawings | Machining and EDM |
| Standard parts BOM | Purchasing |

Steel doors and frames.
Steel doors and fire doors come in endless sizes and options. Width, height, leaves, glazing and finish go in; the elevation, the cut list, the hardware set, the laser profiles and the price come out.
Width 1000 → 1500 mm: single leaf becomes double, hinges re-placed, glazing re-checked, reinforcement and cut list rebuilt, laser profiles of every panel regenerated, price recalculated.
What we automate
| Output | For |
|---|---|
| Elevation drawings | Customer and site |
| Cut lists and BOM | Production |
| DXF panel profiles | Laser and press brake |
Other configurable equipment.
The same platform and the same method, for racking and automated storage, electrical panels, lifts and escalators. Each one opens live in the platform.

Storage and ASRS
Pallet, double-sided and cantilever racking, and pallet ASRS with stacker cranes and P&D conveyors: frames, beams, rails, drives and cycle times from bays, levels and load.
Open in 3D
Electrical panels
Switchgear line-ups, switchboards and motor control centres: sections, doors, busbars and flat patterns.
Open in 3D
Lifts and escalators
Passenger and goods lifts and escalators: shaft, guide rails, car, counterweight, machine and landing doors from load, stops and floor height.
Open in 3D